Clothing Manufacturer for Established Brands and Global Labels
OEM/ODM apparel manufacturing for established brands that need predictable capacity, audit-ready compliance and multi-season continuity across jackets, hoodies, pants, denim and co-ords.
- Multi-season OEM/ODM programs
- ISO-based QC & AQL checks
- Social-compliance, audit-ready
- Vendor consolidation hub
- NDA & artwork/IP protection
- US/UK/EU/CA/AU compliance
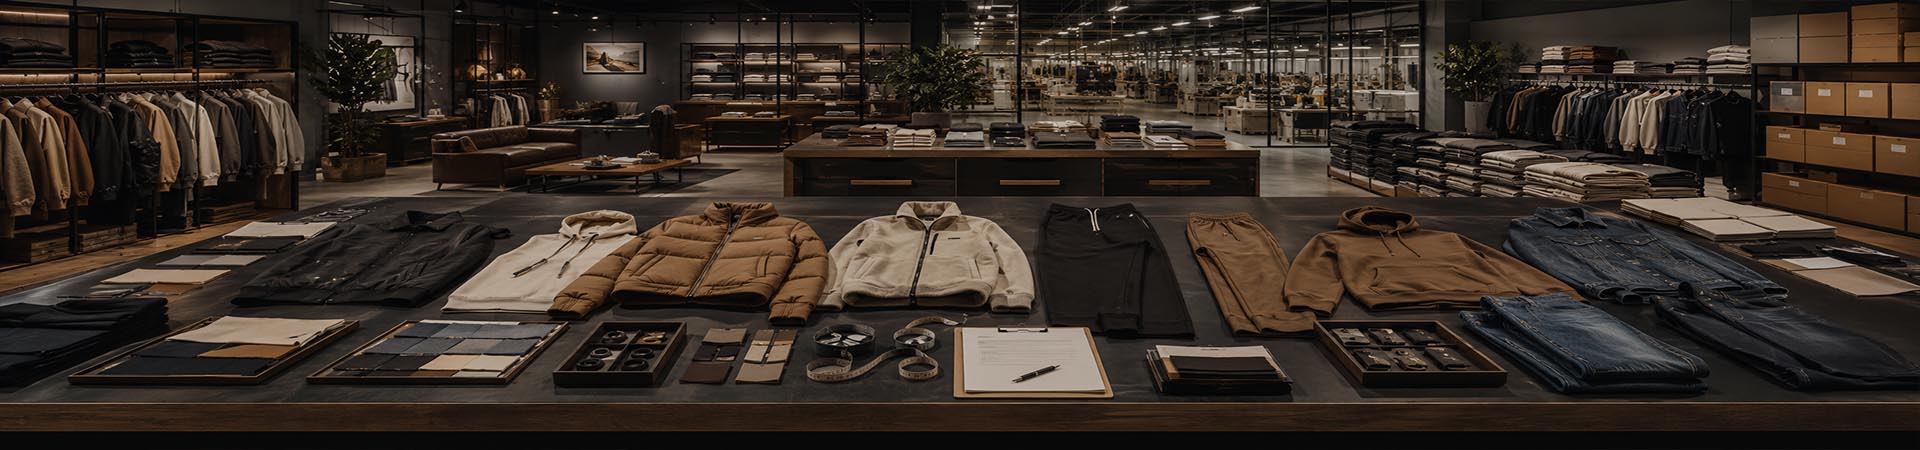
From friction to flow — Your Challenge → Our Solution
Your Challenge
Multi-Season Calendars & Capacity Risk
- Overlapping SS / FW / capsule calendars create constant overlap and compression
- Existing vendors struggle to scale when one category overperforms
- Late capacity visibility makes it hard to confirm buys with confidence
Consistency & Quality Drift Across Seasons
- Same style looks or fits different from one season to the next
- New factories require long learning curves and extra QC resources
- Internal teams spend time firefighting instead of improving the range
Compliance, Audits & Reporting Burden
- Multiple retailers and regions require different audit formats and testing regimes
- Sourcing teams are stuck coordinating corrective actions between factories and auditors
- Compliance failures risk shipment delays or chargebacks
MOQ • Cost • Special Fabrics
- Low‑MOQ quick turns constrained by supply
- Leather/wool/high‑pile extend lead‑time
- Target retail vs cost is hard to align
Assets & Go‑to‑market
- Missing white photos/reels for launch
- Weak drop story & content
- No reliable replenishment mechanism
Our Solution
Structured Capacity Planning & Windows
- Category-based capacity plans aligned to your seasonal calendar
- Reserved production windows for proven styles and families
- Early yardage and trim projections to lock critical paths
- ➤
- Details
Quarterly capacity reviews and shared trackers give sourcing and production teams forward visibility on available slots by category and month.
Category Hubs and Locked Tech Packs
- Dedicated category hubs with stable pattern libraries.
- Locked, version-controlled tech packs for core and carryover styles.
- Inline and final inspections benchmarked against previous approved lots.
- ➤
- Details
We maintain spec histories, PP measurements and photo records so any deviation from previous bulk is flagged early and corrected.
Trend & Fabric Guidance
- Quarterly Trend Pack + Monthly Swatch Drop
- Material Ladder aligned to target retail
- Reference‑to‑Pattern + craft feasibility
- ➤
- Details
Trend PDF sample, fabric ladder tiers and prompt boards.
Dual‑path Quotes & Costed Options
- MOQ 100+ quick‑turn tracks
- Dual‑path quotes: special vs substitute
- Costed options by price tier
- ➤
- Details
Example: leather sleeve vs PU sleeve with lead‑time & MOQ impact.
Pre‑shipment Asset Pack & Lock‑ins
- 5 white photos + 1 mood + two reels
- Launch narrative prompts from Trend Pack
- Lock‑ins: capacity/price windows; pre‑booked trims
- ➤
- Details
Asset deliverables and replenishment cadence templates.
Sample Quote for Established Brands
Choose style → crafts → fabrics → logo size/position to get an instant sample price range and prototype lead‑time. Submit for expert review and alternatives within 24 hours.
Apparel Manufacturing Hubs
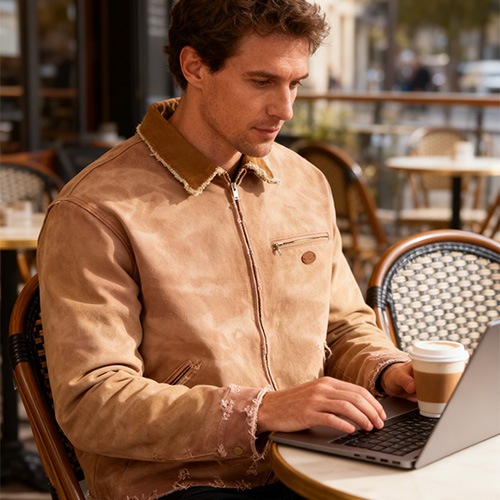
Jackets
Varsity · Bomber · Workwear · Softshell
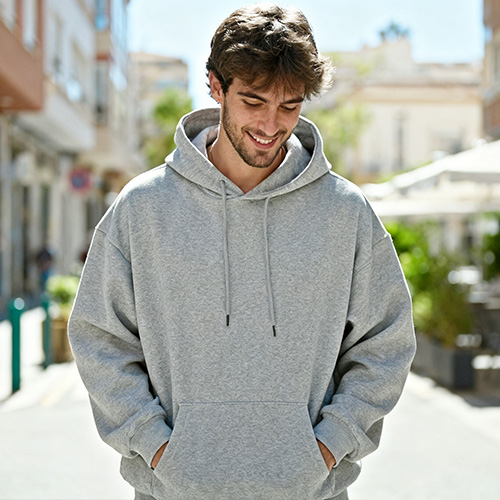
Hoodies
Fleece weights & core fits
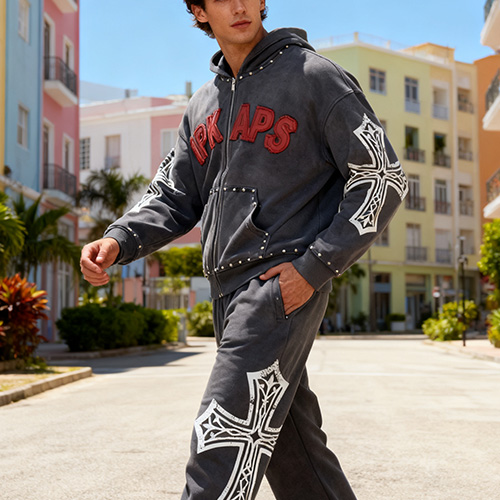
Tracksuits/Sets
Co‑ords for drops
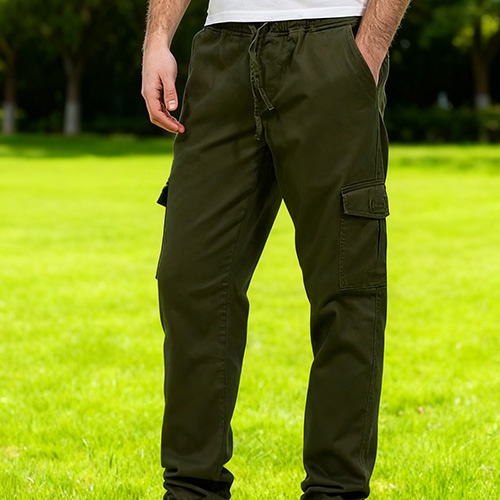
Pants/Joggers
Elastic/zip details
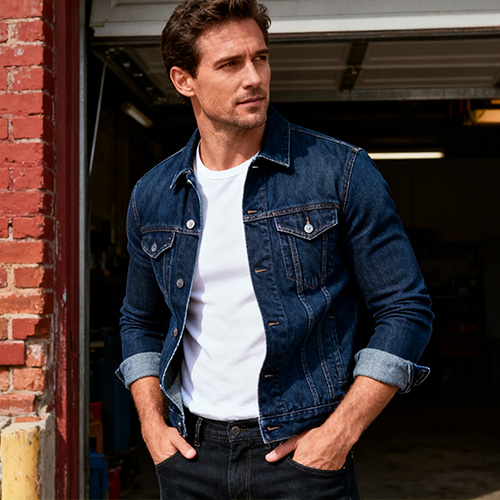
Denim
Controlled washes
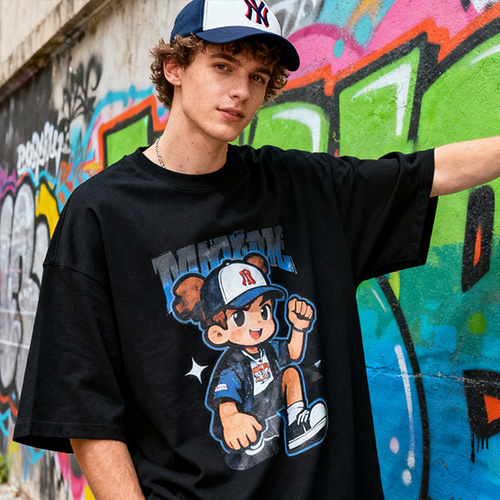
T‑Shirts
Fabric ladders & fits
Established Brand Bundle — Manufacturing Support for Scale
Presale‑ready Visuals
White‑background shots, one mood photo, two 10–15s reels (confidential; never shared without approval).
Trend & Fabric Guidance
Quarterly trend pack + monthly swatch drop; material ladder aligned to target retail.
Dual‑path Quotes & MOQ Guidance
Special vs substitute materials with clear lead‑time/MOQ/price impact.
Replenishment Playbook
Thresholds, capacity/price windows, and pre‑booked trims for fast refills.
Asset & Compliance Spec Sheet
Platform specs, labeling/barcodes/carton marks, and IP guardrails.
Launch Readiness
A checklist & calendar template; we can join review calls with your team/agency.
Anonymized Case Slides & Benchmarks
Proven tactics from similar categories and price tiers.
Optional Social Boost
VANRD channel repost/co‑create (opt‑in, with written approval).
End-to-End SOP & Quality Control
- 1
Fabric Inspection (4-Point)
Check stains/snags/shade/width • Method: 4-Point on machine • Pass: within point limit & shade banding.
- 2
Shrinkage & Wash
Check shrinkage/skew/colorfastness • Method: relax + test wash • Pass: knits ≤3%, wovens ≤2%.
- 3
Print / Embroidery / Chenille
Strike-off approved; color & placement • Pilot-run verify • Pass: placement ±5–8 mm; Pantone match.
- 4
In-line Sewing Audit
FPA; SPI/seams/zipper/symmetry • Hourly audit • Pass: zero critical; SPI per spec.
- 5
End-line Pre-check
Threads/stains/press; hardware safety; key POMs • Operator self-check • Pass: zero critical.
- 6
QC 100% Final
Piece-by-piece workmanship; measurement sampling • Pass: within tolerance; zero critical.
- 7
Pre-pack AQL
Labels/tags/folding/carton marks • AQL Level II • Pass: Cr 0.0 / Ma 2.5 / Mi 4.0.
- 8
Carton Audit
Count & size-ratio; weight & seals • Random recount • Pass: zero mismatch; PSI photos.
SLA & Commitments
| Item | Commitment | Dependencies |
|---|---|---|
| Quote response | ≤ 24 h (workdays) | Qty tiers,destination,category |
| Prototype plan | Dated plan on acceptance | Materials/colours confirmed, payment received |
| Prototype lead-time | 7-10 days | Materials/colours confirmed |
| Bulk plan | Dated plan before PO | PP sign-off, size table locked |
| PP gate confirmation | ≤3 days | Prototype sign-off |
| Pre-shipment assets | >2 days before booking | Style & usage scope confirmed |
| Issue response | ≤24 h first action | Sample/photos/measurement points |
Lock‑in mechanisms (replenishment‑friendly)
- Capacity windowReserve lines for best‑sellers (book in advance)
- Price windowStable price for 30/45 days (except major raw‑material shifts)
- Pre‑booked trimsLabels/ribs/linings archived
- Dual‑path quotesSubstitute materials alongside special fabrics
Signals (anonymized)
- 8 styles in Q1→ 3 replenished in Q2; repeat order rate 42%+
- Prototype on-time 96%; bulk on-time 93% (6-month window)
- PP-to-bulk deviation ≤ ±3% on size points for 95% of lots
- Rework decreased by X% after PP Gate adoption
Metrics from internal ERP & QC logs, 6‑month window; anonymized and available on request.
Capabilities & Scale for Established Brands

Team & Governance
Dedicated owner per brand; cross-functional project squad for key categories; structured check-ins and shared trackers so merchandising, sourcing and QA teams see the same status each week.

Facilities & Equipment
Multi-category factory base with pattern and grading, sampling rooms and production lines, plus partnered washing, printing and embroidery units to support jackets, fleece, pants, denim and knits.

Capacity & Lead‑times
Set up for multi-style programs and replenishment, with quarterly capacity planning, prototype turnarounds typically 7–10 working days and dated ex-factory windows agreed before PO placement.

Quality & Compliance
ISO-referenced quality system with fabric and trim checks, documented AQL inspections and support for social-compliance and chemical-testing frameworks required by major retail and online channels.
10000m²
Production area
568
People
180000pcs+/mo
Capacity (mixed)
25-30days
Fastest case
- Jackets & outerwear
- Hoodies & sweatshirts
- T‑shirts & polos
- Pants & joggers
- Shorts
- Tracksuits & sets
FAQs — Clothing Manufacturer for Established Brands
- What garment labels and compliance documents are required for the US or EU market?Direct answer
For the US: fibre content, country of origin, manufacturer identity (an RN number or name) and care instructions, all permanently attached. For the EU: fibre composition under Regulation (EU) 1007/2011, REACH compliance, and since 13 December 2024 an EU-based responsible person under GPSR. In both markets the legal labeler is the brand or importer, not the factory.
What has to be on the garment
The two markets overlap on fibre and care, then diverge on identity and on who is accountable. The table is the working checklist we use when a label artwork is submitted for approval.
Requirement United States European Union Fibre content Textile Fiber Products Identification Act: generic names and percentages Regulation (EU) 1007/2011: fibre names and percentages, ±3 percentage points tolerance Country of origin Required on imported textile products Origin claims must be accurate; "made in" is not mandatory for all goods Manufacturer identity RN number, or name and address Name and address of the EU responsible person under GPSR Care instructions Care Labeling Rule, 16 CFR 423: washing, bleaching, drying, ironing, warnings ISO 3758 symbols; national rules apply in several member states Restricted substances CPSIA for children's wear; California Prop 65 warning where applicable REACH Annex XVII; GPSR safety and traceability Children's safety Tracking label, lead and phthalate limits EN 14682 drawcord and cord requirements What we need from you before we sew a label
Label content is the brand's legal statement, so we do not draft it. We need the approved artwork, the fibre percentages from the actual fabric and trim composition, the care symbols or text, the RN number or the EU responsible person's details, and the placement and size for each label.
Fibre percentages have to come from the fabric and trim composition, not from the marketing description. A hoodie described as "cotton" with a polyester rib and poly drawcord still has to declare those fibres.
What we produce and what we do not
We sew woven labels, printed care labels, heat-transfer labels and hangtags to the approved artwork, and we can add polybag warnings and carton marks. We check the artwork against the approved fibre list before production, because a label error is a recall risk, not a rework.
What we cannot do is take legal responsibility for the label content. The brand or importer signs the artwork, and that signature is what the factory produces to.
Field example
A US launch of 600 poly-fleece hoodies needed four label elements: 80/20 cotton-poly composition, country of origin, the brand's RN number and four care symbols. The EU sibling order added the GPSR responsible person's name and address, a REACH statement in the technical file, and EN 14682 checks on the drawcord. Artwork was approved in three working days because the fibre list came from the fabric and trim card rather than from the product description.
Numbers that matter
- US: four core label elements — fibre, origin, identity (RN), care
- EU: fibre composition tolerance is ±3 percentage points under Regulation 1007/2011
- GPSR applies from 13 December 2024 and requires an EU-based responsible person
- Care symbols follow EN ISO 3758; keep the approved artwork with the order file
Related questions
- What is the difference between OEKO-TEX and GOTS certification?Direct answer
They answer different questions. OEKO-TEX STANDARD 100 tests the finished article for harmful substances and is granted per product, with no requirement for organic fibre. GOTS certifies organic fibre content and the environmental and social performance of every processing stage, from fibre to finished garment, and requires chain-of-custody documents at each step.
Side by side
A garment can hold OEKO-TEX without a gram of organic cotton, and a GOTS garment also has to meet chemical limits — GOTS includes them, but goes further into fibre, water, energy and labour.
Dimension OEKO-TEX STANDARD 100 GOTS What is certified The finished article and its components The organic fibre and the processing chain Fibre requirement None ≥70% organic; ≥95% for the "organic" grade Chain of custody Not required Required at every stage, with transaction certificates Chemical inputs Tested against limit values Must come from the approved input list Social criteria Not covered Covered, audited annually Validity 12 months, product-specific Annual audit and certification Who holds it The mill or garment maker for that article Each certified operator in the chain What each one is good for
OEKO-TEX is the practical answer for a brand that needs to state the garment is safe against a recognised limit list, including for children's wear through product classes I to IV. It is what a European retailer will normally ask for on a fabric and trim file.
GOTS is the answer for an organic claim. It is also harder to arrange, because every operator in the chain has to be certified and each shipment needs a transaction certificate. A brand cannot decide to "add GOTS" at the packing stage.
How to verify a certificate, and what we can provide
OEKO-TEX certificates carry a number that can be checked in the OEKO-TEX buying guide, and the scope has to name the article or component. GOTS certificates can be checked in the public GOTS database, and the transaction certificate is the document that ties a specific shipment to a certified operator.
Certificates sit with the mill, the printer or the trim supplier that holds them, not with the garment factory. We request the scope that covers your specific fabric, print paste and trims, check that the article description matches, and pass the documents with your order file. We do not describe VANRD as certified for a standard we do not hold.
If a certificate's scope names a different quality code or a different mill, it does not cover your order, even if it is the same fibre.
Field example
A European kidswear brand needed OEKO-TEX product class I for a 320 GSM cotton hoodie. The fabric mill held a certificate covering the quality code, the print paste had a separate certificate from the printer, and the drawcord supplier provided its own. Three documents, one order file. On a later organic programme the same brand moved to GOTS and discovered the fabric mill was not certified, so the order had to be re-sourced before sampling could start.
Numbers that matter
- OEKO-TEX product classes I-IV: baby, direct skin, outerwear, decoration
- GOTS requires ≥70% organic fibre, and ≥95% for the "organic" grade
- OEKO-TEX certificates are valid for 12 months and name the article
- GOTS needs a transaction certificate per shipment, not one certificate per year
Related questions
- How are defective garments handled after inspection or delivery?Direct answer
Handling depends on when the defect is found. In-line defects are repaired at the station and the cause is logged. Units that fail final inspection are sorted 100% and repaired or replaced before packing. After delivery, a claim is checked against the batch code on the carton and the inspection report, and the outcome is replacement or credit depending on whether the fault is ours.
Who handles what, and who pays
The principle is simple: a defect we caused is our cost at any stage; a defect caused after delivery is not. The grey area is wear and wash damage, which is why care labels and wash-test results are kept with the order file.
Stage Action Cost carried by In-line, during sewing Repair at the station, log the cause VANRD Final inspection fail 100% sort, repair or replace before packing VANRD After delivery, production fault Replacement in the next run or credit VANRD After delivery, not a production fault Repair quote or technical advice Buyer What cannot be repaired
Some faults are terminal: a hole in the body panel, a shade that is out of tolerance across the lot, a label with the wrong fibre content, or a decoration that has cured in the wrong position. These are replaced or credited, not repaired, because a repair would still leave a trace the customer can find.
Repairs are also capped. If more than a small share of a lot needs repair, the honest answer is to remake the affected size rather than ship a garment that has been through the needle twice.
Claims and traceability
Every carton carries a batch code that links to the cutting lot, the sewing line and the fabric roll. A claim with a photo and a batch code can be traced in a day; a claim with a photo alone usually ends in a negotiation.
The claim window is set in the contract, typically 30 days from delivery, and decorated styles usually ship with 1-3% spare units so a small number of defects does not become a reorder.
Field example
A 2,400-piece tee order showed 1.8% wavy neck ribs at final inspection, just under the AQL but visible in a retail fold. We sorted 100%, set aside 43 pieces, replaced them from the 2% spare units packed with the order, and changed the rib attaching tension on the next run. No credit was needed and the delivery date held.
Numbers that matter
- 100% sort is triggered when majors exceed the agreed AQL, not when a single defect appears
- 1-3% spare units are standard for decorated styles
- Claim window typically 30 days from delivery, stated in the contract
- Batch code on every carton links to cutting lot, sewing line and fabric roll
Related questions
- What quality control checks matter most for custom streetwear production?
- What causes a custom tracksuit sample to be rejected, and how can brands avoid it?
- Can a third-party inspection company check my bulk order?
- What measurement tolerances are acceptable in bulk clothing production?
- Quality control and inspection at VANRD
- What happens if the delivered bulk order does not match the approved sample?Direct answer
The lot is frozen and compared point by point against the signed approved sample and spec — not against memory or a photo. We quantify how many pieces are affected, trace the cause to a lot, a cutting batch or a process, and then agree a remedy: rework, remake, or a commercial adjustment. Who pays depends on where the fault sits, and the contract decides that.
Step by step
The first 48 hours decide the outcome. If the goods are still in our warehouse the options are wide; once they are in a container or in your warehouse, the practical options narrow to replacement and credit.
Step Action Evidence produced 1. Freeze Hold the lot, stop shipment, segregate by batch Warehouse hold note 2. Compare Approved sample against 3 pieces per size Side-by-side photos, measurement chart 3. Quantify Count affected pieces by colour and size Defect count per carton 4. Trace Fabric lot, cutting batch, sewing line, wash lot Batch records and inspection logs 5. Remedy Rework, remake, credit or rejection Written agreement with dates What counts as not matching
A mismatch is a measurable difference from the approved standard: shade beyond the agreed Delta E, measurement outside the tolerance in the spec, a substituted trim or label, decoration in the wrong position or size, or a fabric hand and weight that no longer matches the approved quality code.
Normal variation inside tolerance is not a mismatch. Garment-dyed styles vary shade across a lot by nature, which is why the tolerance has to be agreed in Delta E before the wash recipe is approved, not after the goods arrive.
How the remedy is decided
If the deviation is a production error on our side, rework or remake is at our cost, and we cover the freight consequence of the delay. If it comes from a change the buyer approved late, from buyer-supplied fabric, or from a wash standard the buyer signed off, the cost is shared or carried by the buyer as the contract sets out.
Either way the remedy is written down with dates before work starts, so there is no second argument about what was agreed.
Field example
A 1,000-piece hoodie order arrived with a shade reading Delta E 2.1 against the approved standard, where the agreed tolerance was 1.0. The cause was a different dye lot of the same quality code. 300 pieces were re-dyed to the standard, the remaining 700 were accepted with a credit per piece, and the mill was put on notice that lot changes must be flagged before dyeing.
Numbers that matter
- Shade tolerance: Delta E ≤1.0 for solid shades, ≤1.5 for garment-washed styles
- Assessment within 48 hours of the claim, with 3 pieces per size compared
- Rework typically takes 7-14 days; remake follows the 25-35 day bulk lead time
- Keep the approved sample and signed spec — without them a claim becomes an opinion
Related questions
- How can brands control sample-to-bulk consistency in custom clothing production?
- How can brands keep hoodie fit, fabric weight, and wash effect consistent across reorders?
- Can a third-party inspection company check my bulk order?
- How do you test garment shrinkage after washing?
- Quality control and inspection at VANRD
- Can I receive an inspection report before my order ships?Direct answer
Yes. Every order produces a pre-shipment report before dispatch, issued as a PDF within 24-48 hours of inspection. It contains the AQL result, the measurement chart against spec, every defect found with photos, the packing and carton data, and a clear pass, conditional pass or fail decision. The order is not released for shipping without it.
What the report contains
The report is written so that someone who has never seen the order can understand what was checked and what was found. It references the approved sample and the signed spec version, because a report against an outdated spec is worse than no report.
Section Contents Order data PO number, style, colourways, size breakdown, quantity Inspection data Date, inspector, AQL level, sample size drawn, cartons opened Measurements 5 pieces per size measured against spec, with pass or fail per point Defects Critical, major and minor counts, location, photo per defect type Packing Pieces per polybag and carton, carton dimensions and weight, shipping marks Result Pass, conditional pass or fail, plus the action required What the result actually means
A pass means the lot met the agreed AQL at the agreed level. It does not mean zero defects — a 2.5 AQL accepts a defined number of majors in the sample by design, and the customer should know that number before the order starts.
A conditional pass means the lot ships only after a named action is completed and evidenced, usually a 100% sort or a specific repair. A fail means the lot is held, and we issue a corrective action with a date.
Who else can see it
The report is yours to forward to your customer or to your own inspection company as a starting point. If you book a third-party inspection, our report and theirs sit side by side, and any difference between them is worth investigating before the container is loaded.
Reports are kept against the order for 12 months, so a claim six months later can be checked against what was actually inspected.
Field example
On an 800-piece jacket order the pre-shipment report flagged 12 majors: the zipper pulls were the right design but the wrong finish, gunmetal instead of matte black. The shipment was held for two days while 800 pulls were replaced from stock and 60 pieces were re-pulled. The re-inspection passed, and the report is what made the difference visible before the goods reached the customer's warehouse.
Numbers that matter
- Report issued within 24-48 hours of inspection, before dispatch
- Standard levels: AQL 2.5 major, 4.0 minor, zero critical
- One inspection day covers up to roughly 3,000 pieces
- Reports retained against the order for 12 months
Related questions
- How can I reduce pilling and fabric wear after washing?Direct answer
Pilling is loose fibres tangling on the surface, so the fix is at the yarn: use combed or combed ring-spun cotton, longer staple, a firmer twist, and brush the inside less. Then confirm it with a Martindale or random-tumble test and accept nothing below grade 3-4. A softer hand-feel and lower pilling pull in opposite directions, so the choice has to be made at sampling.
Where pilling actually comes from
Short fibres escape the yarn during abrasion, roll into small balls and stay anchored to the surface. Carded cotton with a high short-fibre content pills faster than combed cotton, and a loosely twisted yarn releases fibres faster than a firm one. Brushing the inside of a fleece improves the hand-feel but also raises more fibre ends.
Abrasion is not evenly distributed. Underarm, cuffs, the lower back where a bag rubs and the inside of the thigh are where pilling shows first, which is why a wear test on the whole garment hides the problem until the customer finds it.
Lever Effect on pilling Trade-off Combed instead of carded yarn Large reduction, fewer short fibres 5-10% higher yarn cost Longer staple cotton Fewer fibre ends escape Fibre availability and price Firmer yarn twist Binds fibres into the yarn Slightly crisper hand-feel Lighter inside brushing Less surface nap to pill Less immediate softness Anti-pilling finish Measurable improvement Hand-feel and shade can shift Polyester blend Better abrasion resistance Loses natural hand and breathability How to test it before bulk
Two methods cover most buyer requirements. Martindale to ISO 12945-2 runs a set number of rubs, usually 2,000, against a standard abradant. The random tumble test, ASTM D3512, puts the sample in a chamber with cork or pumice for 30 minutes. Both produce a grade from 1 to 5, where 5 is no pilling.
We test on the finished fabric, not greige, because brushing, washing and softening all change the result. For a brushed fleece the inside face is graded separately from the outside, since that is where the customer sees pilling first.
What to write into the spec
Put a grade and a method in the spec, not an adjective. "No pilling" cannot be inspected; "Martindale ISO 12945-2, 2,000 rubs, grade 4 minimum, inside face" can be measured, argued and repeated.
If the brand sells at a premium price point, grade 4 is the realistic target. At volume price points grade 3 is common, and grade 3-4 is a sensible middle.
Field example
A 420 GSM brushed fleece hoodie graded 2-3 on the inside face after five home washes, which the brand's returns data had already flagged. We moved the shell to combed ring-spun cotton, reduced the brushing passes and added an enzyme finish. The next lot graded 4 at 2,000 Martindale rubs, with a hand-feel the brand accepted on the first round.
Numbers that matter
- Pilling scale 1-5, where 5 is no pilling; grade 3-4 is the usual commercial floor
- Martindale test to ISO 12945-2 at 2,000 rubs, or random tumble to ASTM D3512 for 30 minutes
- Combed yarn adds roughly 5-10% to yarn cost and is the single biggest lever
- Grade the inside face of a fleece separately — that is where pilling appears first
Request a Custom Apparel Quote
- FOR You
- *Full Name
- *Phone